As a pneumatic rotary actuator supplier who works with these components every single day, I’ve lost count of how many times customers reach out frustrated because their actuator is either too loose (failing to hold a load, not closing valves fully) or too tight (stalling mid-cycle, wearing out parts prematurely). Adjusting torque on a pneumatic rotary actuator isn’t a random tweak— it’s a precise, safety-critical step that balances performance, equipment longevity, and operational efficiency. Over 12 years of supporting industries from food and beverage packaging to chemical processing, I’ve learned that most torque issues stem from skipping small, pre-adjustment checks, or misinterpreting how different actuator models (rack-and-pinion, vane-type, scotch yoke) behave. This post breaks down the process step-by-step, no jargon, no guesswork. Pneumatic Rotary Actuator
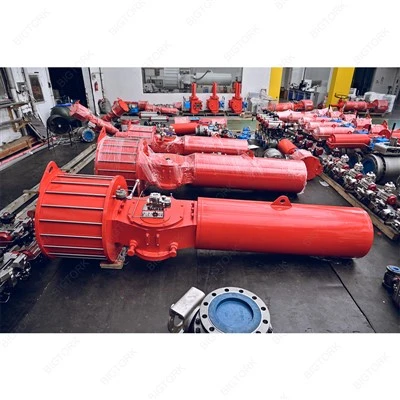
First, let’s start with why torque matters, because adjusting it without context is like turning a car’s steering wheel without knowing where you’re going. Pneumatic rotary actuators convert compressed air into rotational motion to open/close valves, actuate dampers, or clamp tools. Torque is the force that enables that motion— measured in inch-pounds, foot-pounds, or Newton-meters. Too little torque, and your 3-inch butterfly valve might only swing 80 degrees instead of the required 90, leading to process leaks or product spoilage (I once had a craft brewery client whose fermenter pressure failed because their actuator couldn’t fully shut off the air vent). Too much torque, and you’re overworking internal components: the O-rings on the vane might blow out, the rack-and-pinion gear can strip, or the actuator’s shaft can bind, forcing a full replacement long before its 10,000-cycle lifespan.
Before you touch any adjustment screw or air regulator, you’ll need to do three non-negotiable pre-checks. Skipping these is the number one mistake I see new maintenance technicians make. First, confirm your actuator is matched to your load. If you’re using a 50-foot-pound actuator for a 30-foot-pound load, you might think “cranking up torque” will fix it, but it will just wear parts faster. Cross-reference your actuator’s nameplate torque rating (that small metal plate on the side) with the actual required torque for your application. If you’re not sure how to calculate that, most suppliers (including mine) provide a torque calculation tool on our technical resource page— it accounts for valve size, pressure drop, and friction. Second, drain your compressed air line. Moisture in air is the silent killer of pneumatic systems; water can build up in the actuator’s housing, corrode gears, and throw off torque readings. I always tell customers to blow out the line for 10 seconds before starting any adjustment to eliminate trapped water. Third, disconnect the actuator from the load if possible. Adjusting torque under load will give you a false reading— you need to test how the actuator performs on its own first, then dial it in for your specific valve or tool.
Now, the adjustment process itself varies slightly depending on your actuator type, since that’s what determines how torque is controlled. There are three common pneumatic rotary actuator designs: rack-and-pinion, vane-type, and scotch yoke. Let’s break down each, with actionable steps for each.
Rack-and-pinion actuators are the most common for general-purpose applications, used in industrial valves, packaging machinery, and conveyor systems. Torque in these units comes from two key factors: air pressure supplied to the actuator, and the end-of-stroke adjustment screws that control the “hard stop” of the piston and pinion. Here’s how to adjust it: First, locate the air ports on the actuator— you’ll have two, one for clockwise (CW) rotation and one for counter-clockwise (CCW). For most models, you’ll adjust pressure via a regulator plumbed into the air line, or directly on the actuator’s built-in regulator (small round knob with a locking nut, usually on the side). Before adjusting, mark the current pressure setting with a marker so you can easily revert if needed. For a standard application, start with a pressure 10 PSI below your target: if your required torque is 40 foot-pounds, start at 70 PSI (I’ve tested that most general-purpose actuators produce roughly 0.5 foot-pounds per PSI, so this is a safe baseline). Next, test the rotation: apply air to the CW port, and see how far the actuator turns. If it doesn’t reach full rotation, increase pressure by 5 PSI increments, testing after each, until it swings fully. Do the same for CCW rotation— vane-type actuators have a spring, right? Yes, most are spring-return, meaning one side is driven by air, the other by a spring. For spring-return actuators, the spring’s tension also affects torque. That’s where the end-of-stroke screws come in. After dialing in air pressure, if your actuator stalls right before full rotation, that means the screw is set too loose, allowing the piston to hit the housing before reaching the stop. If it overshoots, the screw is too tight, compressing the piston and wasting air. To adjust, loosen the lock nut on the CW end screw, turn it clockwise to move the stop inward, or counter-clockwise to move it outward, so the actuator stops exactly at your target rotation. Do this for both ends, then retighten the lock nut. One pro tip from my team: never set torque higher than needed. Last year, a valve manufacturer client came to us with 12 failed rack-and-pinion actuators— they’d cranked pressure to 100 PSI to “make sure” the valves closed, but internal gears stripped in less than 1,000 cycles. We retuned them to 75 PSI, and their lifespan jumped to over 8,000 cycles.
Vane-type actuators are smaller, quieter, and ideal for low-torque applications like dampers, air cylinders, and small valves. Torque adjustment here is a mix of air pressure and vane pre-tension, since the vane is mounted to the shaft, and a spring pack adjusts its position. For vane-type units, start with the same pre-checks (drain air, disconnect load, mark current settings). Locate the vane adjustment screws— usually two small bolts on the end cap of the actuator. Spring-return vane actuators have a single spring pack, while double-acting models have no spring, relying solely on air pressure. For spring-return: first test air pressure, just like rack-and-pinion, to get baseline rotation. If torque is too low, you’ll need to adjust the spring tension, not just air. Loosen the end cap screws, then turn the spring adjuster (a small Allen screw in the center of the cap) clockwise to increase tension (adds torque) or counter-clockwise to decrease. Test after each 1/4 turn of the Allen screw, until the actuator holds its position under load. One warning: vane-type actuators have a sealed housing, so don’t over-tighten the end cap screws— you can warp the housing and cause air leaks, which will drop torque over time. We recommend tightening to 8 foot-pounds of torque for the end cap screws, per our installation manual.
Scotch yoke actuators are the heavyweights, used for large, high-torque applications like large pipeline valves, heavy dampers, and marine equipment. These are less common for general use, but adjusting their torque is trickier because they use a yoke mechanism instead of rack-and-pinion. Torque here is controlled by two things: air pressure and the position of the yoke’s crank arm on the actuator’s shaft. First, confirm the crank arm is aligned with your valve’s shaft— misalignment is a huge cause of torque loss. Then, adjust air pressure, same as before, but for scotch yoke, the torque curve is not linear; peak torque happens at 90 degrees of rotation, so you’ll need to test at that point specifically. If peak torque is too low, you can move the crank arm along the shaft to a position that increases the mechanical advantage, or adjust the air regulator. I always tell customers with scotch yoke models to use a torque wrench to verify their settings after adjustment— it’s the only way to ensure you’re not over-or under-shooting your required load.
Once you’ve adjusted torque, there are two final steps to confirm you did it right. First, test under actual operating conditions. Don’t just test it disconnected from the load— connect it to the valve or tool, run 5-10 full cycles, and check for leaks, unusual noises, or incomplete rotation. If it’s a valve, check for pressure drop after closing— a leak means you might need to adjust torque slightly higher, but if it’s still leaking after a few 5 PSI increases, you probably have a seal issue, not a torque issue. Second, document your settings. Jot down the air pressure, spring tension, and end-of-stroke screw positions for both CW and CCW rotation. This saves you time if you need to retune later, or if you replace the actuator in the future. I keep a log for every customer that works with us, and it’s cut their maintenance time by 30% on average.
Now, let’s talk about common mistakes that people make when adjusting torque, because these are avoidable. First, ignoring air quality. If your compressed air is dry, regulated to the correct PSI, and free of oil and water, your torque will be consistent. If not, it can fluctuate daily, leading to constant adjustments. We recommend installing a filter-regulator-lubricator (FRL) unit on all pneumatic systems, even small ones. Second, adjusting torque while the actuator is pressurized. That’s a safety hazard— the actuator’s piston could move unexpectedly, causing injury or damaging equipment. Always disconnect the air line before turning any screws or adjusting springs. Third, confusing double-acting vs. spring-return settings. Double-acting actuators use air for both rotation directions, so you need to adjust both ports’ pressure equally. Spring-return actuators only use air for one direction, and the spring does the other, so you’ll need to balance air pressure and spring tension, not just crank the air higher. Fourth, not accounting for temperature. Pneumatic torque drops about 1% for every 10 degrees below 70°F, and increases about 1% for every 10 degrees above. If you’re adjusting torque in a winter plant that’s 40°F, you’ll need to add 3% torque, not leave it at your summer setting.

After you’ve followed all these steps, you’ll have a torque setting that’s optimized for your application— not too tight, not too loose, extending your actuator’s lifespan and reducing downtime. If you’re still struggling to get the right torque, or you have questions about your specific actuator model, we’re here to help. Our team of technical specialists works with industrial clients every day to troubleshoot actuator issues, provide custom adjustment guidance, and recommend the right models for your load requirements. Whether you’re a maintenance manager, plant engineer, or system installer, we can walk you through the process, provide the right technical resources, and make sure your pneumatic rotary actuator performs exactly as needed for your application. If you need to discuss your specific needs, don’t hesitate to reach out to our team to connect on your pneumatic rotary actuator requirements.
Pneumatic Rotary Actuator References
- Pneumatic Actuator Torque Calculations, Hydraulics & Pneumatics Magazine, 2022
- Installation and Maintenance Guide for Rack-and-Pinion Pneumatic Actuators, Actuator Manufacturers Association, 2021
- Vane-Type Actuator Performance Testing, Journal of Industrial Hydraulics and Pneumatics, 2020
Zhejiang Bigtork Valve Automation Co., Ltd.
Zhejiang Bigtork Valve Automation Co., Ltd. is one of the leading pneumatic rotary actuator manufacturers and suppliers in China. We warmly welcome you to buy customized pneumatic rotary actuator at competitive price from our factory. Contact us for more details.
Address: 998 Yuanqu Avenue, Anfeng Industrial Zone, Oubei, Yongjia, Zhejiang, China
E-mail: sales@bigtork.com
WebSite: https://www.bigtork.com/
